As a steel drilling supplier who’s spent 12 years on the floor, working alongside rig crews, metallurgists, and quality control teams, I’ve learned that the work we do—drilling steel—isn’t just about turning metal into a precise part. It’s about balancing speed, precision, and safety, because every year, I see crew members who walk away from jobs with preventable injuries, or teams that have to pause operations because a drilling mishap damaged expensive equipment. When people ask me what the biggest risks are, I don’t just list generic OSHA bullet points. I talk about the hazards I’ve watched play out, the small oversights that turn into big problems, and the gaps even experienced teams miss. The truth is, drilling steel’s hazards aren’t always obvious—they hide in the way we choose bits, set parameters, or even ignore that one strange noise a machine makes mid-job. Let’s break down the real, actionable hazards, because that’s what keeps my own team (and our customers’ teams) safe. Drilling Steel
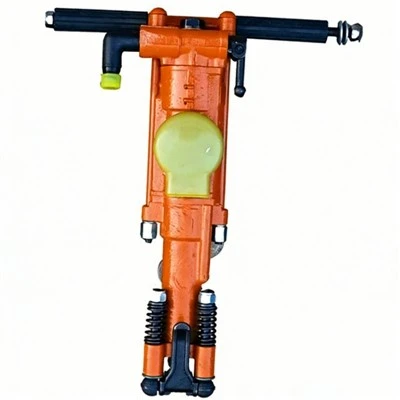
First, the most immediate hazard everyone knows about but underrates: flying debris and high-velocity metal chips. When you’re drilling into steel—whether it’s mild carbon steel for construction, alloy steel for heavy machinery, or stainless steel for medical equipment—each rotation of the drill bit chips off tiny, razor-sharp pieces of metal. At typical drilling speeds, those chips can fly at 200 feet per second, fast enough to penetrate safety glasses, slice through skin, or even cause eye damage that leaves a worker permanently blind. Last year, a customer of mine in the Midwest cut corners on their chip collection system: they skipped replacing a clogged conveyor on their drill press, so metal chips kept piling up and bouncing off the machine guards. One chip ricocheted off a hidden seam in the steel they were drilling, hit a worker’s unprotected cheek, and required 12 stitches. The worst part? The worker said they’d checked their PPE that morning, but their safety glasses had a scratch that let a chip slip through. Even minor wear on eye protection can create a gap large enough for a chip to pass through. And it’s not just the chips themselves: when you drill hard steels, like tool steel or high-strength low-alloy (HSLA) steel, the chips can be hot enough—up to 1,500°F for some high-speed drilling—to cause thermal burns if they land on exposed skin or clothing with loose folds. I’ve seen a rig operator’s sleeve catch a pile of hot chips, and by the time he noticed, his arm had second-degree burns. The fix isn’t just “wear safety glasses”—it’s ensuring chips are contained with automatic shrouding, PPE is inspected daily, and crews don’t wear loose sleeves or jewelry that can snag on rotating parts.
Next up, a hazard that’s often overlooked because it doesn’t make a loud noise: exposure to metalworking fluids (MWFs) and airborne metal dust. MWFs are the liquids we use to cool drill bits, lubricate the cutting zone, and flush away chips—they’re essential, but they’re also a slow-moving hazard. Most MWFs are made with mineral oils, synthetic chemicals, or even soluble oils that can harbor bacteria when they’re not properly maintained. Over time, these bacteria produce mists that workers breathe in, leading to skin irritation, respiratory issues, and even occupational asthma. I had a long-time customer in automotive manufacturing whose MWF tank hadn’t been tested in 18 months; three of their drill operators developed persistent coughs that required respiratory therapy. Worse, some MWFs contain volatile organic compounds (VOCs) that evaporate into the air, causing headaches, dizziness, and long-term organ damage with repeated exposure. Then there’s the airborne metal dust itself: when you drill steel, fine metal particles break off and become suspended in the air. Respirable crystalline silica isn’t the only risk here—iron dust, specifically from ferrous steels, can build up in the lungs, leading to siderosis, a condition that scar tissue over time and impairs breathing. For teams drilling stainless steel, which contains chromium and nickel, those dust particles can trigger allergic reactions or more severe respiratory conditions. The key here is MWF maintenance: regular pH testing, proper filtration, and replacement on schedule, not just when it starts smelling bad. Also, local exhaust ventilation (LEV) systems above drill stations aren’t a luxury—they’re a requirement for keeping dust and mists out of the air. I always advise my customers to test their air quality quarterly, not just rely on the machine’s built-in filters.
Then there’s the silent killer of drilling operations: the risk of machine and tool failure leading to catastrophic injury or structural damage. Drill bits aren’t one-size-fits-all, and using the wrong bit for the steel you’re drilling is a recipe for disaster. For example, using a high-speed steel (HSS) bit on HSLA steel, which has a higher tensile strength than mild steel, will cause the bit to overheat, dull quickly, or even shatter mid-drill. I saw this happen on a pipeline project a few years ago: a crew tried to drill 4-inch holes in 2-inch thick HSLA steel with regular HSS bits, no coolant, and one bit shattered. The shrapnel flew through a gap in the machine guard, hit a worker in the torso, and landed 15 feet away. The damage didn’t stop there: the broken bit also nicked the drill press spindle, requiring $12,000 in repairs and a two-week delay to the project. Even when bits don’t shatter, improper drilling parameters—like too much feed rate or too low spindle speed—can cause the drill bit to “walk” off the intended hole location, leading to slips, falls, or damaged workpieces. I’ve had customers drill through a support beam by accident because their bit walked, leading to a structural shift on a construction site that required the entire area to be evacuated for 8 hours. Another tool failure risk is the drill chuck: if a chuck isn’t tightened properly before drilling, the bit can come loose mid-operation, spinning wildly and hitting nearby workers or equipment. Last year, a small fabrication shop I supply lost a $50,000 CNC drill because a chuck came loose while drilling a 6-foot steel plate, slamming the bit into the machine’s frame. Preventing this isn’t just about buying the right drill bit—it’s about training crews to match bits to steel grades, calibrate machine parameters daily, and perform pre-use inspections of chucks, guards, and spindle speeds. We even provide our customers with a free drill bit selection guide, tailored to the steel grade and application, because we’ve seen too many mistakes come from guessing which bit to use.
One hazard that’s unique to drilling steel, especially when working with large or thick steel sections, is ergonomic strain and cumulative trauma disorders (CTDs). Most people think of drilling hazards as immediate injuries, but CTDs are the ones that cripple workers over years of work. When you operate a drill press, especially a hand-held one, you’re exerting repetitive force on your wrists, elbows, and shoulders. For crews drilling 100+ holes a day, the constant pushing and twisting to feed the drill can lead to carpal tunnel syndrome, tennis elbow, or rotator cuff injuries. I have a close friend who worked as a drill operator for 20 years; he retired last year after having two rotator cuff surgeries because he’d adjusted his grip on his drill to handle the weight, leading to constant strain. Even on automated drilling machines, there’s ergonomic risk: workers who load heavy steel plates onto drill tables can suffer back injuries if they don’t use proper lifting techniques or mechanical aids. Last quarter, a customer of mine in agricultural manufacturing had a worker slip a disc while lifting a 500-pound steel beam onto a drill table—he was out of work for three months, and the company paid over $20,000 in workers’ comp. The fix here isn’t just ergonomic desk chairs; it’s training for proper lifting, rotating drill tasks between workers to reduce repetitive motion, and investing in lifting aids like magnetic lifters or hoists for heavy steel loads. I always emphasize to my customers that safety isn’t just about avoiding accidents—it’s about keeping workers healthy for the long haul.
Finally, there’s the hidden hazard of electrical and fire risks, which often get overlooked because drilling steel is a “cold” process compared to welding or cutting. But when you have high-power drill presses, often running on 480-volt circuits, near flammable materials like wood shavings, oil-soaked rags, or even the MWF itself, fires can start quickly. A few years ago, a job site in Texas had a fire that destroyed two drill presses and 10 tons of steel stock; the cause was a frayed electrical cord on a drill machine that sparked, igniting a pile of oil-soaked chips left near the machine. The fire department said it took just 90 seconds for the flames to spread across the chip pile to the steel pallets, which burned intensely for two hours. Electrical shocks are another risk: if a drill machine is not properly grounded, or a worker’s hands are wet from spilled MWF, they can receive a serious shock. I’ve heard of a worker who was drilling steel on a wet floor and got shocked, falling off a ladder and breaking his leg—all because the machine’s ground fault interrupter (GFI) had been bypassed for a few weeks because it was “inconvenient.” The key here is regular electrical inspections of drill equipment, keeping work areas dry and free of flammable debris, and never bypassing safety features like GFIs or emergency stop buttons.
Coupling As a steel drilling supplier, my job isn’t just to sell high-quality drill bits and steel stock—it’s to help my customers avoid these hazards, because I know firsthand that a safe job site is a profitable job site. Every hour a crew is down due to an injury, every piece of equipment damaged by a preventable mistake, every worker who misses time due to an occupational illness hits the bottom line. That’s why I spend as much time walking job sites, talking to crews, and sharing safety tips as I do on the phone taking orders. If you’re a fabrication shop, construction team, or manufacturing plant working with drilled steel, and you want to review your current drilling processes, inspect for hazards, or find the right steel and drill bits tailored to your application, I’m here to help. We offer free on-site consultations for our clients, tailored safety checklists for drilling steel, and product recommendations that balance quality and safety. Don’t let preventable hazards put your crew or your project at risk—reach out to connect, and let’s build a safer, more efficient drilling operation together.
References
- Occupational Safety and Health Administration (OSHA). 2023. "Metalworking and Machining Hazards." U.S. Department of Labor.
- National Institute for Occupational Safety and Health (NIOSH). 2022. "Occupational Exposures to Metalworking Fluids: A Review of Health Effects." Centers for Disease Control and Prevention.
- American National Standards Institute (ANSI). 2021. "Safety Standard for Machine Tools: Drill Presses." ANSI/B11.1-2021.
- Society of Manufacturing Engineers (SME). 2020. "Drilling Safety Best Practices for Ferrous and Non-Ferrous Metals." SME Press.
Super Rock Machinery Equipment (Qingdao) Co., Ltd.
We are one of the most professional drilling steel manufacturers and suppliers in China, featured by quality products and good price. Please feel free to buy advanced drilling steel for sale here from our factory. Welcome to view our website for more information.
Address: No. 45, Pengwan Road, Qianwan Bonded Port Area, Qingdao Sub-district, Free Trade Pilot Zone, Shandong China
E-mail: sales@superrocktools.com
WebSite: https://www.superrocktools.com/
