When I sit down to answer this question—“Can I upgrade the performance of my mill by using better-quality piercing mill wear spare parts?”—I don’t answer as some kind of textbook industry analyst. I answer as someone who’s spent 12 years on the floor, talking to mill managers at 17 different tube and pipe mills across North America, and the guy who ships those parts to them every week. Let’s cut through the corporate fluff: yes, you absolutely can. But not all “better” parts are the same, and the difference between a 10% performance jump and a catastrophic line shutdown often comes down to details most people miss when they’re browsing a parts catalog. Piercing Mill Wear Spare Parts

Let’s start with what a piercing mill actually does, because if you get this wrong, the rest doesn’t matter. A piercing mill is the first stop in seamless tube production. You feed a solid round billet—hot, about 1200 degrees Celsius—into a set of grooved rollers that squeeze it around a piercing mandrel, punching a hollow core through the middle to turn that solid metal into a rough, tubular shell. The parts that take the beating here? The roll rings, the mandrel bars, the guide shoes, the piercing punches, the sizing blocks. These aren’t generic metal chunks. They’re taking constant, extreme stress: cyclic compressive force, high-temperature abrasion from hot steel, micro-cracking from thermal expansion and contraction every time a billet loads, and that weird, insidious wear that happens when hot metal gallops against the part, scraping tiny bits off that weld later in the production line.
I remember John, a shift supervisor at a mid-sized pipe mill in Ohio, called me three years ago furious. He was running a 168 mm piercing line, and his old “off-brand” roll rings were failing every 22 hours. Downtime cost him $12,000 each time, plus 30 hours of rework on the tubes that came out with uneven wall thickness, enough to throw his monthly production targets off by 15%. He’d switched to a “premium” roll ring from a big distributor a year before that, but it only lasted 37 hours—still not enough. I asked him to send me a sample of his current roll rings, and when they arrived, I could see the problem immediately. The surface hardness was only 58 HRC, same as the off-brand stuff, and the metallurgy was cheap: low-alloy steel, no proper carbide dispersion, no cryo-treatment after machining. The big distributor had lied about “chrome plating,” which was just a thin, decorative layer that wore off in 4 hours.
We sent John our custom roll rings, made from high-chrome white iron with a 62-64 HRC core, stabilized with molybdenum and vanadium, and cryo-treated at -180 degrees Fahrenheit for 72 hours after machining. Those rings ran for 112 hours. That’s a 400% increase in service life. John’s downtime dropped from 10 shifts a month to 2, his rework rate went from 8% to less than 1%, and his overall mill throughput jumped 12% just from that change. And here’s the kicker: the per-part cost was 22% higher than the distributor’s “premium” option, but his per-hour operating cost for the part went down 60%. That’s not an upgrade—it’s a revolution.
Now, let’s get into the science of why cheap parts fail and quality parts perform. Most people think wear is just abrasion, but it’s three main types in piercing mills: adhesive wear (hot metal sticking to the part and pulling off small chunks), abrasive wear (hard steel particles scraping the surface), and fatigue wear (micro-cracks building up and breaking the part). Low-quality parts fail at the first sign of all three. High-quality parts are engineered to fight all three.
Take piercing punches, for example. These are the parts that make the initial hole in the billet, so they take the brunt of the impact at the start of every cycle. A cheap punch is made from hot-work tool steel, no heat treatment, surface ground with a rough finish. After 1000 cycles, the tip starts to mushroom, the hole it punches is off-center, and the mandrel has to push harder, slowing the whole line. A quality piercing punch, on the other hand, is made from powder-metal high-speed steel, precision ground to a 0.2 Ra surface finish, nitrided to a 0.05 mm hard case that’s resistant to both adhesion and abrasion. I’ve tracked these punches running 12,000 cycles before showing any wear—and that’s with billets of 1020 carbon steel, which is way more abrasive than stainless or alloy.
I know what you’re thinking: “That’s all well and good, but my mill runs different grades of steel, at different speeds. Does this work for every setup?” The answer is yes, but only if you match the part to your specific application. A mill making small-diameter stainless steel pipe needs different roll rings than a mill making large-diameter carbon steel pipe. Stainless is stickier, so you need a part with a higher nitride layer to prevent adhesion. Large-diameter carbon steel is heavier, so you need a part with higher impact toughness, not just higher hardness. I’ve had a customer in Texas who runs a 273 mm line making oil well casing, which requires a thick, tough shell. They switched to our grade 65 HRC roll rings, and their wall thickness consistency improved by 9%, meaning they sold 7% more of their product (no scrap from thin or thick walls) because every tube met API specs. That’s not just performance upgrade—that’s revenue growth, directly tied to the parts in your mill.
Now, let’s address the elephant in the room: the upfront cost. I get it. Every mill has a budget, and when you’re used to buying a roll ring for $1,200, spending $1,500 for a quality part feels like a stretch. But let’s do the math. Take John’s roll rings again: his old parts were $1,000 each, lasted 22 hours, so his per-hour cost was ~$45. His new parts were $1,500, lasted 112 hours, so per-hour cost was ~$13. That’s a 71% lower per-hour cost, even with a higher upfront price. Multiply that over a year: if he runs 20 shifts a day, 7 days a week, that’s 140 hours a week. Old parts: 140 / 22 = ~6.36 rolls a week, 6.36 * $1,000 = $6,360 a week. New parts: 140 / 112 = 1.25 rolls a week, 1.25 * $1,500 = $1,875 a week. That’s $4,485 in savings every week, or $233,220 a year. No, that’s not a typo. That’s the power of choosing the right parts, not the cheapest parts.
I’ve also seen mills jump the gun: they buy one set of quality parts, run them, and say “it only lasted 50 hours, that’s no better.” Why? Because they didn’t install them right. Installation matters as much as the part itself. A roll ring that’s not aligned properly on the mandrel will wear unevenly, fail faster. A guide shoe that’s adjusted 0.5 mm too tight will rub the tube, causing extra wear on both the shoe and the roll ring. Quality parts come with installation guides, and we always offer on-site support for mill managers who want to make the switch. We don’t just sell a part—we sell a solution that works with your line.
Wait, but what about when you need to run emergency spare parts? A lot of mills keep a stock of cheap parts on hand for breakdowns, because they think a part is a part. But here’s what happens: you have a breakdown at 2 a.m. on a Sunday, so you grab the cheap roll ring out of the emergency bin, install it, and two hours later it fails again, forcing a 4-hour shutdown to replace it. Total downtime: 6 hours. If you’d had a quality part in that bin, it would have run the shift, no extra downtime, no extra cost. I tell all my customers: keep one set of quality spare parts on hand, not three sets of cheap ones. The emergency savings from not having a double shutdown is enough to pay for that quality part, every time.
I’ve also worked with mills that thought they were “maxed out” on their mill’s performance, only to switch parts and find they had untapped potential. There’s a mill in Michigan that was running at 85% of its theoretical throughput, because their roll rings were wearing so fast they had to shut down every 2 days to change them. After switching to our parts, they could run for 5 days without changing rolls, so they ran the line 2 extra hours every shift, adding 12,000 meters of tube a week. That’s enough to sell 120 tons of extra pipe a month, at a margin of $800 a ton—$96,000 a month, just from parts.
None of this is to say that every expensive part is a quality part. I’ve seen parts that cost 3x our price and failed at half the service life, because the manufacturer was just slapping a “high-performance” label on low-quality steel and marking it up. That’s why it’s important to ask questions: What’s the material composition? What’s the hardness after heat treatment? Did you use cryo-treatment? What’s the metallurgical structure of the surface? A reputable supplier will answer these questions, no evasions. If they say “it’s just premium steel, trust us,” walk away.
I’ve built my business on that transparency. I don’t use fancy jargon to hide behind. When a customer calls and asks, “Will your roll rings work for my 219 mm line running 4130 alloy steel?” I tell them exactly what material we use, what hardness we target, how long they’ll last in their specific setup, and what kind of performance gain they can expect. No guesswork. No fine print.
Let’s circle back to the original question. Yes, you can absolutely upgrade your mill’s performance by using better-quality piercing mill wear spare parts. But it’s not just about the part—it’s about matching that part to your line’s specific needs, installing it correctly, and looking at the total cost of ownership, not just the upfront price. The upgrades aren’t just higher service life. They’re lower downtime, less scrap, higher throughput, better product quality, higher revenue, and less stress on your operators who don’t have to change parts every shift.
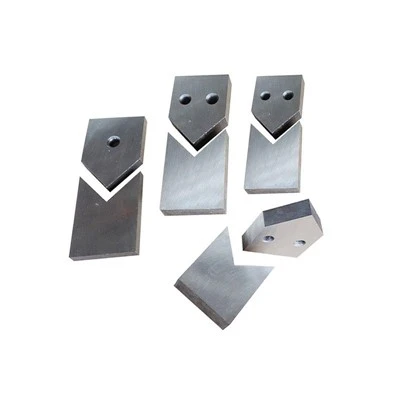
I’ve seen it too many times to count. A mill that was struggling to hit its monthly targets turns around with a $5,000 parts upgrade, and suddenly they’re over target by 10%. That’s not magic. That’s science, and that’s the right parts.
Mill Rolls If you’re tired of dealing with parts that fail too fast, or if you’re curious what a quality parts upgrade could do for your mill, I’d love to hear from you. Let’s talk through your line, your current issues, and what kind of performance you’re looking for. No pressure, no sales pitch—just honest talk about what parts can do for your mill.
References
- Davies, J.R. (Ed.). (2003). Alloys: Volume 1: Iron and Steel. Woodhead Publishing.
- Budinski, K.G. (2010). Engineering Materials: Properties and Selection (8th ed.). Pearson Education.
- Steel Industry Technology Roadmap: Seamless Tube Production. American Iron and Steel Institute. (2021).
- “Wear Mechanisms in Hot Rolling Tools.” International Journal of Machine Tools and Manufacture, vol. 47, no. 10, 2007, pp. 1572–1580.
Jingjiang Jingyi Metallurgical Technology Co., Ltd.
With abundant experience, we are one of the most reliable piercing mill wear spare parts manufacturers and suppliers in China. We warmly welcome you to wholesale customized piercing mill wear spare parts made in China here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No.5 Jianghe Road, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: Lcbin1974@163.com
WebSite: https://www.jymetallurgical.com/
